Aluminium vs Stainless Steel vs Titanium
The three materials that cover most machined parts, compared on the numbers that actually decide the choice — specific strength rather than raw strength, and total machined cost rather than price per kilogram. If the part doesn't need metal at all, our plastic machining guide covers the polymer route.
The Short Answer
- Weight matters (aerospace, moving robot axes, anything on a gantry) → titanium first, 6061 aluminium when budget rules.
- Weight doesn't matter, corrosion or wear does → stainless, and it will usually be the cheapest of the three to machine.
- Neither is critical → 6061-T6 aluminium. It is the default for a reason: cheapest stock, fastest to cut, easiest to finish.
The rest of this page is the reasoning, because the decision is rarely that clean.
| Property | 6061-T6 Aluminium | 304 Stainless | 316 Stainless | 17-4PH Stainless | Ti-6Al-4V Titanium |
|---|---|---|---|---|---|
| Density (g/cm³) | 2.70 | 8.00 | 8.00 | 7.80 | 4.43 |
| Yield strength (MPa) | 276 | 215 | 205 | 1,100 | 880 |
| Tensile strength (MPa) | 310 | 505 | 515 | 1,310 | 950 |
| Specific strength (yield ÷ density) | 102 | 27 | 26 | 141 | 199 |
| Elastic modulus (GPa) | 68.9 | 193 | 193 | 197 | 113.8 |
| Thermal conductivity (W/m·K) | 167 | 16.2 | 16.3 | 18 | 6.7 |
| Max service temperature (°C) | ~200 | ~870 | ~870 | ~315 | ~400 |
| Corrosion resistance | Good (anodised) | Very good | Excellent (marine) | Good | Excellent |
| Relative material cost | 1× | 3–4× | 4–5× | 6–8× | 10–20× |
| Relative machining time | 1× | 3–5× | 3–5× | 4–6× | 5–10× |
| Machinability | Excellent | Moderate — work hardens | Moderate — work hardens | Difficult | Difficult — heat + reactivity |
| Biocompatible | No (usually) | Yes | Yes | Sometimes | Yes — excellent |
| Magnetic | No | No (annealed) | No (annealed) | Yes | No |
Values are typical for the tempers shown and vary by supplier and heat treatment. Specific strength is yield strength divided by density — higher means more strength per unit of weight.
Sources & Notes
Every figure in the table is a typical room-temperature value compiled from published reference sources, not an original measurement. When a property is load-bearing, work from the mill test report for the lot you actually receive. Primary references:
- ASM Handbook, Volume 2 — Properties and Selection: Nonferrous Alloys and Special-Purpose Materials, plus Volume 1 for the stainless grades. Yield, tensile and specific-strength values.
- MatWeb Material Property Data — density, elastic modulus and thermal conductivity per UNS designation (A96061, S30400, S31600, S17400, R56400).
- ASTM B348 / AMS 4928 (Ti-6Al-4V) and ASTM A276 / A479 (stainless bar) — specification limits by product form.
Relative material cost and machining-time factors are order-of-magnitude indicators consolidated from the same references and current mill pricing, expressed as multiples of 6061-T6 aluminium — confirm with a live quote for the specific grade and form. Specific strength = yield strength ÷ density.
Last updated: 2026-10-03.
Why Specific Strength Is the Number That Matters
Pull one figure out of that table: specific strength — yield strength divided by density.
Titanium scores about 199, 6061 aluminium about 102, and 304 stainless about 27. Read that as: for the same weight of material, titanium carries roughly twice the load of aluminium and over seven times the load of 304 stainless.
This is why the "titanium is strongest" claim is both true and misleading. Titanium's absolute yield (880 MPa) is actually lower than heat-treated 17-4PH stainless (1,100 MPa). Titanium wins on strength per kilogram, not strength per square millimetre.
So the first question isn't "how strong does it need to be" — it's "how strong does it need to be per kilogram?" If the part sits on a bench and never moves, the answer doesn't matter and stainless or aluminium will be far cheaper. If it's on the end of a moving robot arm, every kilogram you remove is payload you gain.
What Each Material Is Like on the Machine
6061-T6 aluminium — the default for a reason
Cuts fast, holds tolerance easily, takes a beautiful anodised finish, and costs the least per kilogram of the three. Thermal conductivity is high (167 W/m·K), so cutting heat leaves with the chip instead of cooking the tool.
Where it stops working: above roughly 200°C it loses a large share of its room-temperature strength. It's relatively soft, so bare aluminium galling and wear are real issues in sliding contact. And it needs anodising or plating for saltwater exposure.
We published a full comparison of the common aluminium grades if you've settled on aluminium and just need to pick the alloy.
304 and 316 stainless — cheap material, expensive machining
The trap here is that stainless stock is only three to five times the price of aluminium per kilogram, so it looks like a modest step up. It isn't, because the machining time is three to five times longer — so the finished part can cost several times more, not the three-fold the material price suggests.
Why it cuts slowly: austenitic stainless work-hardens rapidly. A tool that rubs instead of shearing makes the surface harder for the next pass, and it compounds. Combined with poor thermal conductivity (16 W/m·K, a tenth of aluminium), heat stays in the tool.
316 vs 304: 316 adds molybdenum, which is what makes it the right choice for marine and chloride environments. If your part isn't seeing saltwater or harsh chemicals, 304 is cheaper and machines the same.
17-4PH is a completely different animal — a precipitation-hardening grade that reaches 1,100 MPa yield after heat treatment. That's stronger than Ti-6Al-4V in absolute terms. It's used when you need very high strength without paying titanium prices, and you can tolerate the weight.
Ti-6Al-4V — excellent material, genuinely difficult to cut
Three things compound to make titanium slow and expensive on the machine:
- It barely conducts heat — 6.7 W/m·K, about one twenty-fifth of aluminium. Cutting heat has nowhere to go except into the tool edge, which is why titanium destroys cutting tools.
- It's chemically reactive at cutting temperature and can weld itself to the tool edge, then tear pieces out of it.
- Low elastic modulus means the workpiece deflects away from the cutter under load, then springs back — you get chatter and rubbing instead of a clean shearing cut.
We wrote a full titanium machining guide covering speeds, tooling, tapping and the chip fire risk. What that means in practice: lower cutting speeds, rigid setups, sharp tooling changed early, and constant flood coolant. We run it regularly and it's perfectly manageable — just budget for the cycle time honestly. How machining cost is calculated covers why cycle time dominates the quote.
Where titanium earns its cost: aerospace structures, medical implants (it's the most biocompatible of the three), and anywhere the strength-to-weight ratio is the entire point of the design.
Seven Questions That Pick the Material
| Ask yourself | If yes |
|---|---|
| Is the part weight-critical or on a moving axis? | Titanium first, aluminium if budget rules |
| Does it run above 200°C in service? | Rule out 6061 — stainless or titanium |
| Is it implanted or in contact with body tissue? | Titanium, or 316 stainless |
| Seawater, chlorides or harsh chemicals? | 316 stainless or titanium; anodised aluminium marginal |
| Sliding wear without surface treatment? | Stainless over bare aluminium |
| Non-magnetic required? | Rule out 17-4PH (it's magnetic) |
| None of the above applies? | 6061-T6 — cheapest and fastest |
Three Mistakes We See Repeatedly
1. Specifying titanium when aluminium would do
Titanium sounds like the premium, safe choice. But if the part isn't weight-critical, you've multiplied the cost of the part by five to ten for a property nobody is using. Ask what the weight saving actually buys you — if the answer is "nothing measurable," it's 6061.
2. Choosing stainless by material price alone
Stock price says stainless is 3–4× aluminium. Finished-part cost says several times more, because the cycle time is 3–5× longer. Budget on the machined part, not the bar.
3. Treating "stainless" as one material
304, 316 and 17-4PH differ enormously — 316 for chlorides, 17-4PH when you need 1,100 MPa yield, 304 for general use. Writing "stainless steel" on a drawing leaves the shop guessing, and they may quote a grade that doesn't suit the application.
Four Specification Gaps We Flag on Incoming RFQs
The mistakes above are about picking the wrong material. These are narrower — a drawing that names a material but leaves out the one detail that decides whether the part actually works in service. None of them needs a different metal; each needs a single line changed on the drawing. We flag all four before quoting, because the corrected part costs the same to make and a great deal less to fix later.
1. "Stainless steel" with no grade, intended for outdoor or marine use
A shop will quote the cheapest grade that satisfies the words on the drawing — almost always 304. 304 is perfectly good indoors, but it pits in chloride environments: road salt, coastal air, process chemicals. If the part lives outside or near the sea, that 304 part fails early. The fix is a one-word change: specify 316. We never let a marine-environment part go out quoted as plain "stainless steel."
2. 6061 specified where 7075 would have been safer
6061-T6 yields about 276 MPa. For a bracket under shock or repeated load, many drawings simply say "aluminium" with no temper at all — which leaves the actual strength open to whatever the shop happens to stock. Designers often don't realise 7075-T6 reaches roughly 503 MPa yield, nearly double, at a small step up in cost. Where the load demands it, the lever is naming the temper and, if needed, the grade.
3. Anodising called out on an alloy that anodises poorly
Anodising takes a clean, protective coat on the 6xxx series (6061, 6082) and most 5xxx. But 2xxx (2024) and 7xxx (7075) anodise to a muddy, uneven finish because of their copper and zinc content, and the layer is less protective. A drawing that says "anodised 7075" is effectively asking for a cosmetic reject. Where a wear-resistant coating is needed on those alloys, we steer to a different surface route rather than fight the chemistry.
4. Hard-coat anodise on a tight-tolerance feature
A Type III (hard) anodise layer adds material to every surface — typically tens of microns per side under MIL-A-8625. If a bore or shaft is called out to a tight tolerance and then hard-anodised, the coating can push the finished size out of spec unless the machined dimension was pre-compensated for the coating thickness. We always check whether post-coat dimensions were accounted for before quoting, because the alternative is a scrapped batch that looked perfect on the drawing.
Material Selection Questions
Which is stronger: aluminium, stainless steel or titanium?
Why is titanium so expensive to machine?
Is stainless steel harder to machine than aluminium?
When does aluminium stop being a good choice?
Can I substitute stainless for titanium to save cost?
What about plastics — should I consider POM or PEEK?
Which material is cheapest to machine overall?
Which is best for corrosion resistance and marine use?
Tell Us the Application, Not Just the Material
Send the drawing with a line about where the part lives — load, temperature, environment, whether it moves. We'll tell you if the specified material is right, over-specified, or wrong for the application, and quote alternatives side by side.
Related: Material Selection Guide
Related industries: CNC Machining for Automotive · CNC Machining for Aerospace
Cite this page
Used this in a report, quote justification or internal standard? A link back helps other engineers find the same reference. Suggested anchor text — reword freely:
<a href="https://www.ataimeisen.com/stainless-vs-aluminum-vs-titanium.html">Aluminium vs Stainless Steel vs Titanium — FSCPRECISION</a>
No permission needed. Please do not rehost the page — link to it instead so the numbers stay current.
Embed this chart
The whole decision on one page — decision tree, the numbers that decide, and the three costly mistakes. Drop it into a blog post, course page or internal standard; it links back here.
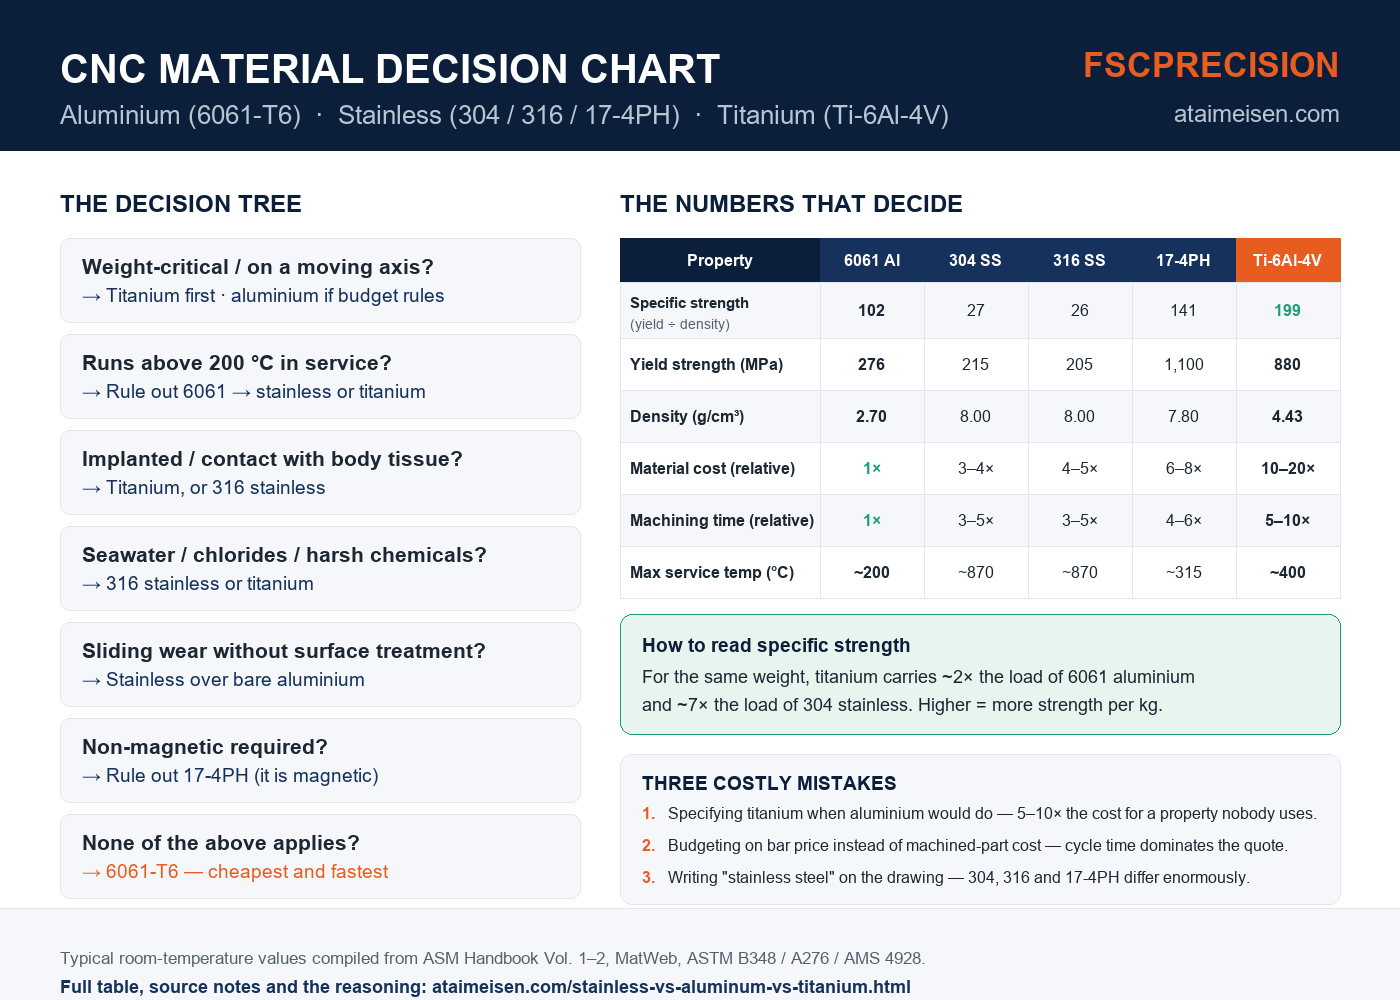
Download PNG for use in slide decks or printed handouts.
